A refinery supervisor in Peru rang us about numbers that refused to add up. Crude entered one end, packed product left the other, and the gap ran wider than anyone had warned him. Nothing dripped onto the floor. The missing volume was leaving dissolved in stuff he paid to discard.
Shrinkage across a refinery is neither mystery nor bad luck. Product escapes along four routes, and every one can be weighed. Name them first.
Four exits, and what each one takes
Gums go out first, during the hydration step. Phosphatides drag good triglycerides with them, particularly when water dosing is rushed or measured by eye.
The heavy phase follows, if you neutralize with lye. It separates readily and pulls saleable material down behind it.
Saturated earth leaves third, holding what it adsorbed in its pores. Then the stripper adds its share, since live steam sweeps volatiles away and entrains a little good glyceride on the ride out.
That's the whole map. Which door dominates depends on what arrives at your gate and how the shift runs the unit.
FFA and the soap phase: usually the biggest single door
Caustic turns free fatty acids to soap. That phase is denser, it settles, and it takes triglycerides with it. Your raw material arrives carrying a certain acid load, so you manufacture a predictable quantity of soapstock, and the bottoms carry product out through the separator.
Over-treating makes it worse. Surplus reagent attacks neutral material directly, saponifying what you meant to sell. Mills running a fixed dose regardless of incoming acidity do this constantly, and nobody notices, because the giveaway is smeared across every batch and never shows up as one dramatic event.
Clay leaves wetter than it arrives
Dry powder goes in. Bleaching earth saturated with glyceride comes out. Those pores hold far more than most operators assume, and the cake resting in your filter press retains a surprising volume.
Three levers help. Charge the media to the colour you actually need rather than a habit. Give the filter time to drain properly. And look at recovering what's in spent cake instead of burying it.
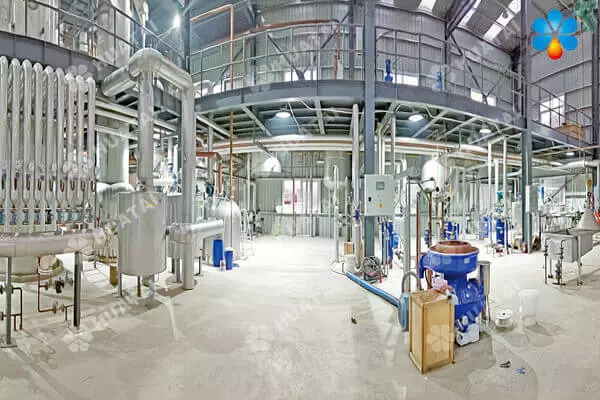
Our oil refining equipment section covers the hardware behind each of these stages.
Physical versus chemical: two different loss profiles
Physical refining skips lye entirely, distilling fatty acids out under vacuum with steam. On high-acid crude that closes the soapstock door altogether, which is why mills handling rice bran or palm often go this way.
It isn't free. This route demands much cleaner gum removal and colour treatment, since you forfeit the cleaning that neutralization provides. The stripper also works harder, so what leaves as distillate climbs.
Chemical refining makes a heavy phase but tolerates messy raw material. The question isn't which route shrinks less in the abstract. It's which route suits what shows up at your gate.
The deodorizer is quieter than most people assume
Nobody watches this one closely, and they should. Live steam strips odours and acidity, and it inevitably sweeps some saleable glyceride out with the vapour. Push temperature too high, pull vacuum harder than the spec needs, or run steam faster than necessary, and you pay for it every hour the vessel is warm.
Our soybean oil production line page shows where deodorizing sits in a complete configuration.
Finding your own biggest leak
Weigh and sample every outgoing stream. Gums, soapstock, spent earth, distillate. Set the total against what entered, and you'll know your split within a shift or two.
Guessing is what costs people. One plant we walked blamed its deodorizer for months. Measurement showed most of the gap came from a caustic dose nobody had revisited since commissioning.
Feed quality sets the floor beneath all of this: acidity, phosphatides, moisture and suspended solids decide how much you must strip out before anything is saleable, and no amount of careful operating downstream recovers material that reached your gate already spoiled.
Five operating changes worth making
Charge caustic against measured acidity. Not against last month's recipe.
Take the hydration step seriously. Proper water dosing, plus acid or enzymatic conditioning where it pays, cuts what leaves in the gums.
Tune earth dosage to colour. Over-bleaching wastes media and product together.
Run the stripper as gently as your spec allows. Surplus heat and steam cost you continuously.
Store crude cool and dry. Acidity climbs in storage, and every point it gains becomes soapstock later. Our palm oil production line page covers storage and handling for high-acid material.
Common mistakes we keep meeting
Fixed caustic dose regardless of raw material. What arrives changes; your rate should too.
Never weighing outgoing streams. You can't manage a number nobody records.
Chasing a colour target with more earth. Try better gum removal first.
Overrunning the deodorizer "to be safe". That caution has a running cost.
Buying cheap media. Poor filtration leaves more glyceride in the cake than the saving is worth.
FAQ
What causes the biggest refining loss?
Usually the soap phase, especially on crude with a heavy free fatty acid load. Caustic converts those acids to soap, and the heavy phase carries triglycerides out with it. Over-treating with surplus reagent saponifies saleable product on top of that. Gums, spent earth and column distillate account for the remainder.
Is physical refining always lower loss than chemical refining?
No. Physical refining closes the soapstock exit entirely, which suits acidic material such as rice bran or palm. It demands far cleaner degumming and colour treatment, and the deodorizer works harder, so distillate rises. Chemical refining gives up more to soap but tolerates variable crude far better.
How do I measure refining loss in my own plant?
Weigh and sample every outgoing stream: gums, soapstock, spent bleaching earth and deodorizer distillate. Compare that total against what entered the refinery and you'll have your split within a shift or two. Measuring beats estimating, because the dominant exit is rarely the one operators suspect.
Does spent bleaching earth really carry much oil?
Yes, more than most operators assume. Bleaching earth enters dry and leaves with its pores saturated. Three things help: dose it to the colour you actually need, let the filter drain fully, and consider recovering what's in spent cake rather than disposing of it.
Planning a refinery, or chasing product you can't account for? Tell us your crude, its acidity, and how far you refine. We'll say plainly where the gap is likely sitting. WhatsApp +86 18337263319. No charge for the read. Chat with us on WhatsApp →