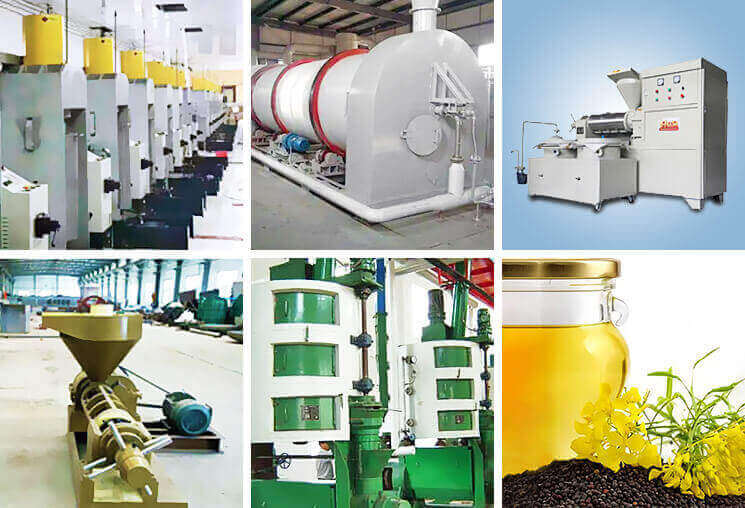
A two-stage rapeseed processing line designed for a Russian agricultural cooperative, combining pre-pressing and solvent extraction to maximize oil recovery from high-oil-content rapeseed.
Russian rapeseed at 38-40% oil content is on the high end of commercial oilseeds. To maximize efficiency, the line uses pre-pressing to recover about 65% of the oil mechanically (which avoids over-loading the extractor), then solvent extraction to bring residual oil in meal down to under 1%.
The line is engineered for cold climate: outdoor-insulated pipework, electric heating for solvent storage, redundant control valves for the cold-weather startup sequence. The control room includes remote monitoring so our engineers can troubleshoot from Hua County when local support is not available.
The line is designed to flex to winter rapeseed, spring rapeseed, and canola. Switching between grades requires only a flaking roll gap adjustment — process parameters for the extractor and DTDC are pre-loaded in the PLC and selected by the operator at HMI.
After two full production seasons, the line has hit 108% of nameplate capacity, with meal at 0.7-0.9% residual oil — among the best in the industry for rapeseed extraction.